Guide to choosing an industrial unit cooler (part 1): efficiency, thermodynamics and longevity
In an industrial refrigeration plant, the evaporator is the component that determines the real thermo-hygrometric conditions of the refrigerated environment and, consequently, the quality of preservation and the system’s overall energy efficiency.
While compressors and condensers define the energy balance of the refrigeration cycle, it is the industrial evaporator that translates its performance into temperature stability, spatial uniformity, humidity control and operational continuity of the cold chain.
An incorrect selection does not only generate a theoretical deviation from the rated data, but produces measurable effects in operation:
- increased defrost frequency
- reduced actual output due to excessive frost formation on the finned pack
- higher specific consumption (kWh/ton)
- thermo-hygrometric instability in the cold room
In medium- and large-scale logistics or food plants, these dynamics easily translate into tens of thousands of euros a year in additional operating costs.
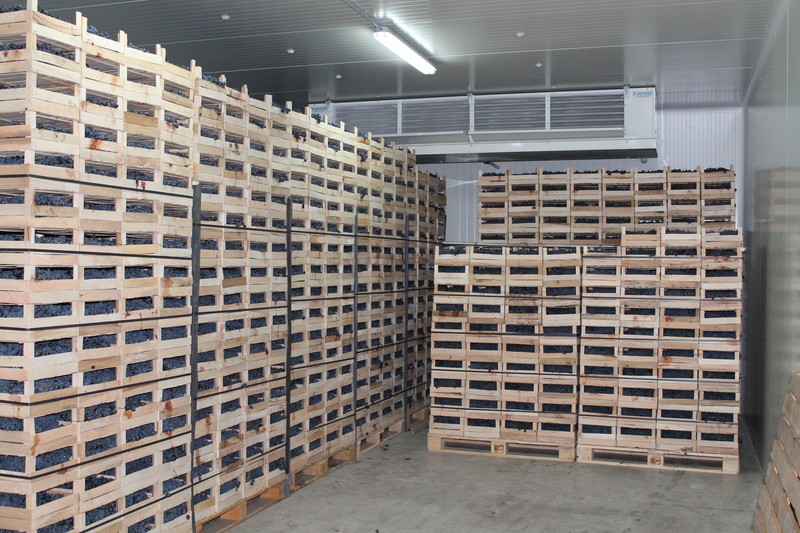
For this reason, choosing an industrial unit cooler cannot be limited to the nominal capacity. It must start from real design data: dynamic thermal load, cold-room usage profile, required humidity, storage layout, refrigerant and defrost strategy.
In this first deep-dive we analyse the sizing principles and the relationship between ΔT, air dynamics and preservation quality. In the next, we will examine the impact of natural refrigerants (CO₂, NH₃, secondary fluids) and the design implications on the plant’s life cycle.
ΔT: the number that decides quality
The thermal power exchanged by an evaporator is expressed by the relationship:
Q = k × A × ΔTₗₙ
where:
- k is the overall exchange coefficient
- A is the finned surface
- ΔTₗₙ is the logarithmic mean temperature difference
At the selection stage, the truly strategic parameter is therefore the operating ΔT, understood as the difference between the air temperature entering the evaporator and the refrigerant’s evaporating temperature.
ΔT is not just a calculation value. It is the variable that connects sizing, energy efficiency and product protection.
High ΔT: compactness and energy penalty
A high ΔT (8–12 K or above) reduces the surface needed to obtain the required capacity. The evaporator is more compact and the initial CAPEX can decrease.
From a thermodynamic standpoint, however, a higher ΔT implies a lower evaporating temperature. For the same condensing temperature, the thermal lift on the compressor increases, with the consequent:
- reduction in COP
- increase in specific absorption
- rise in energy OPEX
The effect is not marginal: a few °C less of evaporation can significantly affect the plant’s annual consumption.
On the air side, a colder surface intensifies dehumidification, accelerates frosting in LT applications and reduces relative humidity in medium-temperature rooms.
In environments for storing fresh meat or fresh produce, this can translate into weight losses of 1–2% in a few days, with a direct impact on margins. Here ΔT is not just an energy parameter: it is an economic variable.
Low ΔT: thermo-hygrometric stability and efficiency
Working with low ΔT (5–7 K) requires more finned surface and therefore larger units. However, it allows operation with higher evaporating temperatures, improving the refrigeration cycle’s efficiency.
This results in:
- better average seasonal COP
- a lower tendency to frost (and a consequent reduction in defrost frequency)
- greater relative-humidity stability (often >85-90% in MT rooms for fresh product)
In applications sensitive to dehydration, a low ΔT represents a design choice oriented to product protection and cold-chain stability.
Packaged and frozen product: a change of priority
In the case of packaged or frozen product, sensitivity to dehydration is reduced. The priority shifts towards:
- available specific capacity
- compactness of the unit
- effective management of high loads
In these contexts, higher ΔT can be technically acceptable, provided the overall energy assessment is consistent with the usage profile.
Even in LT, however, ΔT affects the frosting rate and therefore the share of time devoted to defrosts. An evaporator that spends a significant part of its operating cycle defrosting reduces its own average effective output, with a direct impact on OPEX.

The risk of oversizing
If a high ΔT can penalise energy efficiency, the opposite choice can also be critical.
Indiscriminately increasing the surface to reduce ΔT can lead to:
- insufficient airflow
- poor induction
- thermal stratification phenomena
- non-uniform distribution in the cold room
An oversized evaporator does not automatically guarantee better performance. The design balance must simultaneously consider the exchange surface, air dynamics, evaporating temperature and real operating conditions.
| Parameter | ΔT 8 K or above | ΔT 5–7 K |
| Evaporating temperature | Lower | Higher |
| Impact on COP | Reduction in COP | Improvement in COP |
| Required exchange surface | Smaller | Larger |
| Evaporator size | More compact | Larger |
| Relative humidity in the cold room | Tends to decrease | More stable (>85-90% in MT rooms for fresh product) |
| Frosting rate (LT) | Faster | Slower |
| Defrost frequency | Higher | Reduced |
| Impact on OPEX | Higher energy consumption and defrost costs over the medium term | Lower specific consumption and better average seasonal efficiency |
| Suitable applications | Packaged and frozen product | Fresh meat, fresh produce, sensitive products |
The geometry of air: flow dynamics and unit-cooler configurations
The mechanical configuration of an industrial unit cooler affects not only the footprint or installation. It directly affects the quality of the air-side exchange, and therefore the power actually transferred to the environment.
The relationship assumes that the air passes uniformly through the coil. If the distribution is irregular:
- the overall coefficient k varies locally
- the effective temperature difference is not uniform
- the real output deviates from the nominal one
Flow dynamics are an integral part of sizing.
Large-volume rooms: throw and static pressure
In industrial cubic evaporators for logistics warehouses or deep rooms, volumetric flow alone is not enough. What matters is the combination of:
- airflow
- available static pressure
- useful throw (air throw)
In environments over 10–15 metres deep, throws above 25–30 m are often needed to avoid longitudinal gradients and dead zones.
If the residual static pressure is not adequate to offset the pressure losses generated by shelving or pallets, the flow shortens, recirculation occurs and the room develops thermal stratification.
The result is not just non-uniformity: it is a reduction in the actual cooling output, because part of the volume does not participate correctly in the exchange.

Processing rooms: distribution and comfort
In food processing rooms, air dynamics must reconcile cooling, comfort and hygiene.
The dual-flow configurations distribute air symmetrically, reducing direct draughts on operators and improving mixing. Here the design combines:
- uniform thermal distribution
- acoustic containment
- prevention of localised condensation
Freezing tunnels: overcoming pressure losses
In the blast freezer, air dynamics become decisive.
Densely stacked pallets generate high pressure losses. To rapidly cross the critical crystallisation zone (-1 °C / -5 °C), product velocities of 2–4 m/s are required.
Here the evaporator design must ensure:
- distribution uniformity
- adequate static pressure
- flow-rate stability over time despite frosting
The product’s microstructural quality depends directly on air dynamics.

Choosing a unit cooler cannot be reduced to a rated figure. Variable loads, layout constraints, stringent hygrometric requirements and specific operating conditions demand an integrated vision.
Refteco designs industrial unit coolers integrated into the refrigeration cycle, not components isolated from the plant context. Sizing starts from real process data and integrates:
- rigorous thermodynamic calculation
- operating-ΔT optimisation
- study of flow dynamics
- configuration consistent with the application
If you are designing or upgrading a plant, bring us your process data: correctly sizing an evaporator can become a measurable competitive advantage.

REFrigeration TEchnological COmponents
For more information